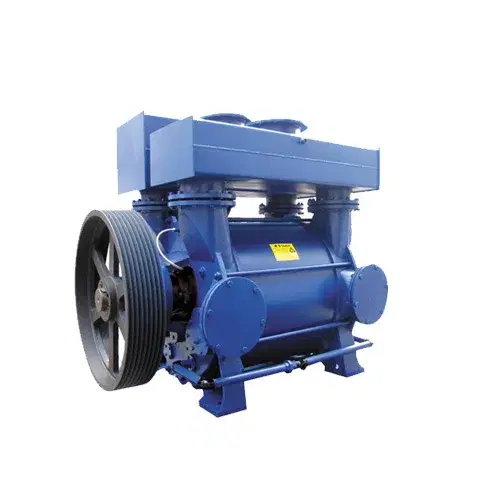
High-Capacity Liquid Ring Vacuum Pump
High-capacity single-stage liquid ring vacuum pump for paper, chemical and mining plants needing very large gas flows.
- Max Capacity
- 2,300 – 62,400 m³/h
- Ultimate Vacuum
- 160 mbar
- Type
- Single-stage liquid ring
- Impeller
- One-piece stamped
Highlights
- Genuine equipment supplied with warranty
- Professional installation & commissioning
- 24/7 after-sales support nationwide
- Genuine spare parts stocked locally
The 2BE3 series scales the single-stage liquid ring principle up to very high capacities — from about 2,300 to 62,400 m³/h — for paper-making, chemical, petrochemical, light industry, pharmaceutical, metallurgy and fertiliser plants. PTFE valve plates replace traditional ball valves to prevent over-compression and automatically adjust the exhaust area, while a one-piece stamped impeller and an integrated gas-water separator improve efficiency and reliability.
You May Also Need
Related Products
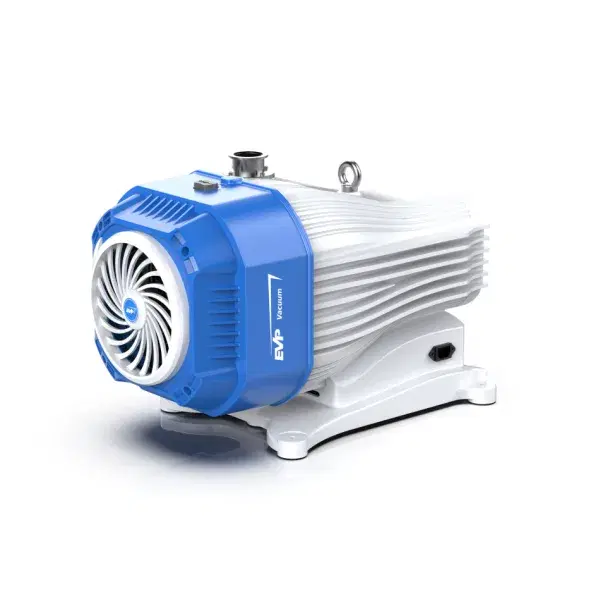
Dry Scroll Vacuum Pump
Completely oil-free and water-free scroll vacuum pump for clean applications such as labs, semiconductors and medical equipment.
View details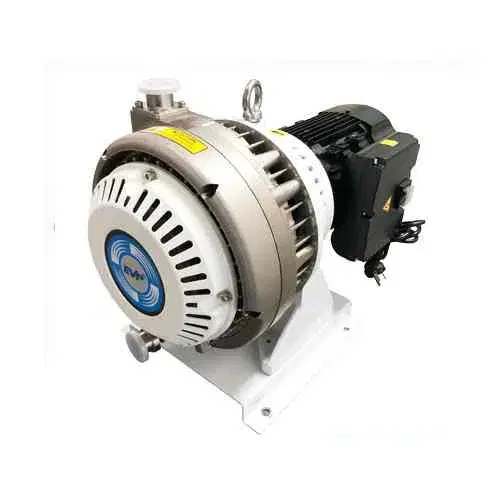
Dry Scroll Vacuum Pump (16 – 60 m³/h)
Higher-capacity oil-free scroll vacuum pump for clean industrial and laboratory vacuum from 4.4 to 16.6 L/s.
View details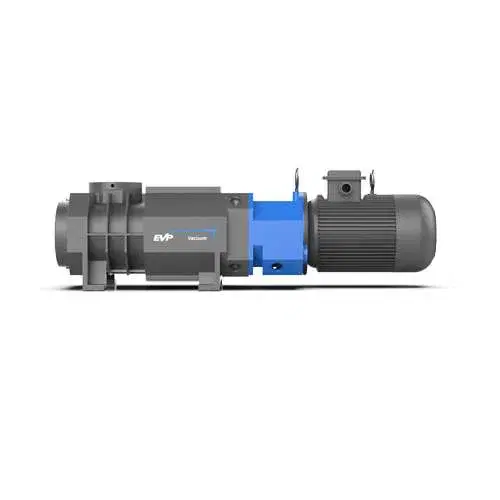
Dry Screw Vacuum Pump
Oil-free dry screw vacuum pump that handles condensable vapours and solids without residue for chemical and process duty.
View details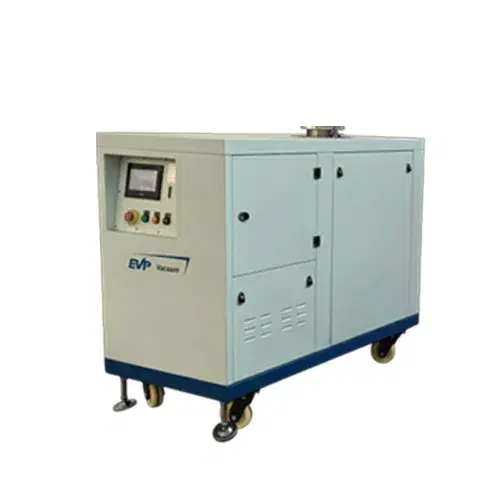
Boxed Dry Screw Vacuum Pump
Enclosed, mobile-framed dry screw vacuum pump with side-panel connections and optional PLC/WiFi monitoring.
View details